In the demanding landscape of modern industrial machinery, the integrity of sealing systems is paramount to operational safety and efficiency. Mechanical Rubber Seals serve as the critical barrier that prevents the leakage of vital lubricants and protects internal components from the ingress of contaminants, ensuring that high-precision equipment functions without interruption. From food processing lines to heavy-duty hydraulic systems, these components are the unsung heroes of mechanical stability.
The global demand for high-performance sealing solutions has surged as industries move toward higher pressures and more extreme temperature environments. The challenge lies in selecting a material that can withstand chemical degradation while maintaining a perfect seal under both static and dynamic conditions. Failure to implement a high-quality seal often results in costly downtime, environmental hazards, and increased maintenance overhead.
By leveraging advanced materials like food-grade silicone, Mechanical Rubber Seals provide a versatile solution for a wide array of applications. Whether it is creating a labyrinth gap to prevent oil leakage or sealing gases in a vacuum, the right rubber seal ensures longevity and reliability for various mechanical equipments across the globe.

Understanding the Fundamentals of Mechanical Rubber Seals
At its most basic level, a rubber seal ring is an annular cover designed to create a tight interface between two components. In the context of Mechanical Rubber Seals, this often involves fixing the seal to a bearing ring or washer. By contacting another ring, the seal forms a narrow labyrinth gap that effectively blocks the exit of oil and the entry of foreign debris, which is essential for maintaining the purity of the internal environment.
These components are engineered to operate under a vast spectrum of conditions, ranging from completely static installations to high-speed moving parts. The ability to seal different liquids and gases under specific temperature and pressure parameters makes them indispensable in the assembly of complex mechanical equipment, ensuring that the system remains airtight and leak-proof throughout its lifecycle.
Industry Relevance and Global Standards
The global industrial sector relies heavily on the standardization of sealing components to ensure interoperability and safety. International standards, such as ISO and ASTM, provide the framework for the dimensions and material properties of seals, ensuring that a part manufactured in one region fits perfectly into a machine in another. This standardization is critical for the maintenance of global supply chains and the reduction of operational risks.
In the manufacturing of rubber parts, the shift toward specialized materials has allowed industries to push the boundaries of what is possible. For instance, the use of food-grade silicone in seals is not just a preference but a regulatory requirement in pharmaceutical and food processing industries to prevent contamination. This intersection of material science and regulatory compliance defines the current state of high-end rubber seal production.
Challenges such as thermal expansion and chemical corrosion continue to drive innovation. When a seal fails in a critical system—such as a hydraulic press or a pneumatic valve—the result is not just a leak but a potential safety hazard. Therefore, the industry focuses on "zero-failure" engineering, where the durability of the rubber compound is tested against the most extreme predicted operating conditions.
Core Functional Components and Design
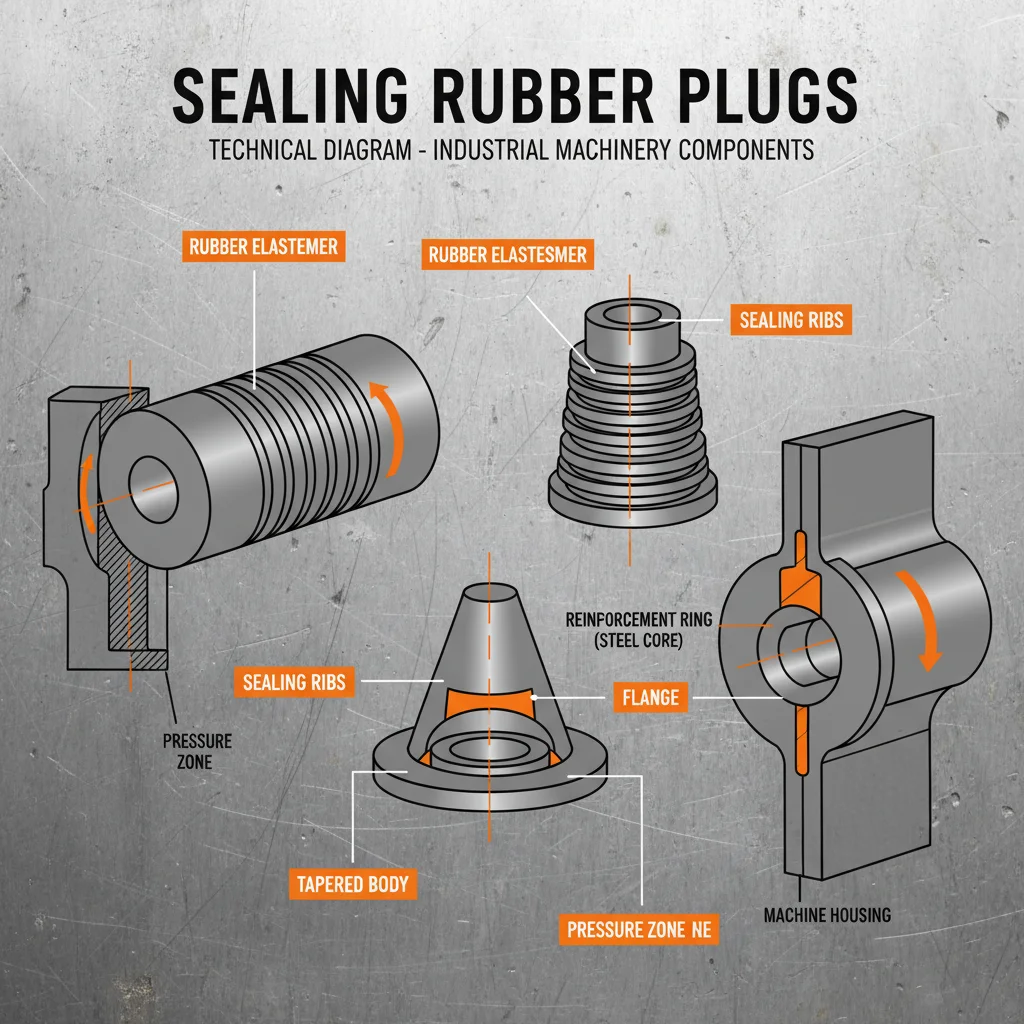
The efficacy of Mechanical Rubber Seals depends largely on the geometry of the annular cover and the precision of its fit. The design must account for the "labyrinth effect," where a complex path is created to hinder the movement of fluids. This design philosophy ensures that even under fluctuating pressures, the seal remains seated and functional.
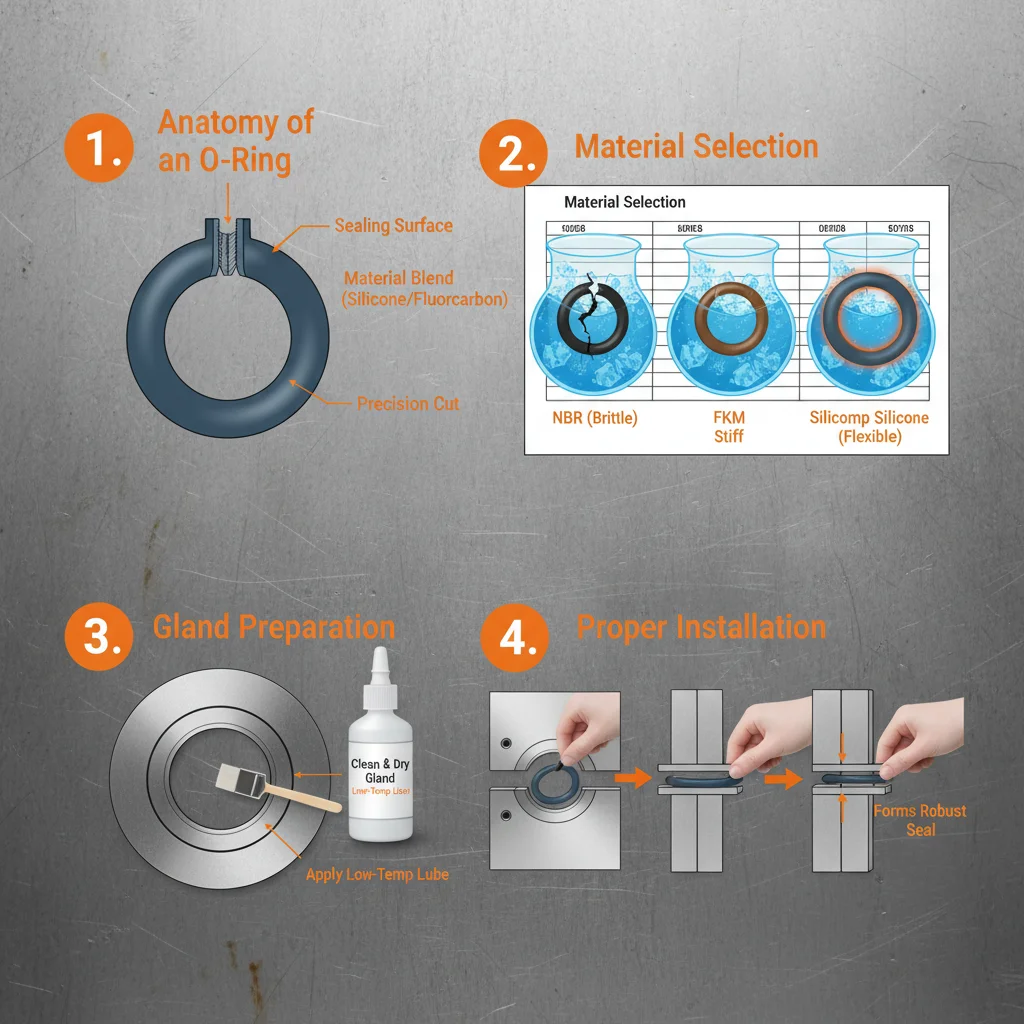
Material selection is the second pillar of design. For Mechanical Rubber Seals intended for food-grade applications, colored silicone is often used to allow for easy visual identification and to meet non-toxic standards. The elasticity of the rubber allows it to conform to microscopic surface irregularities on the metal rings, creating a truly hermetic seal.
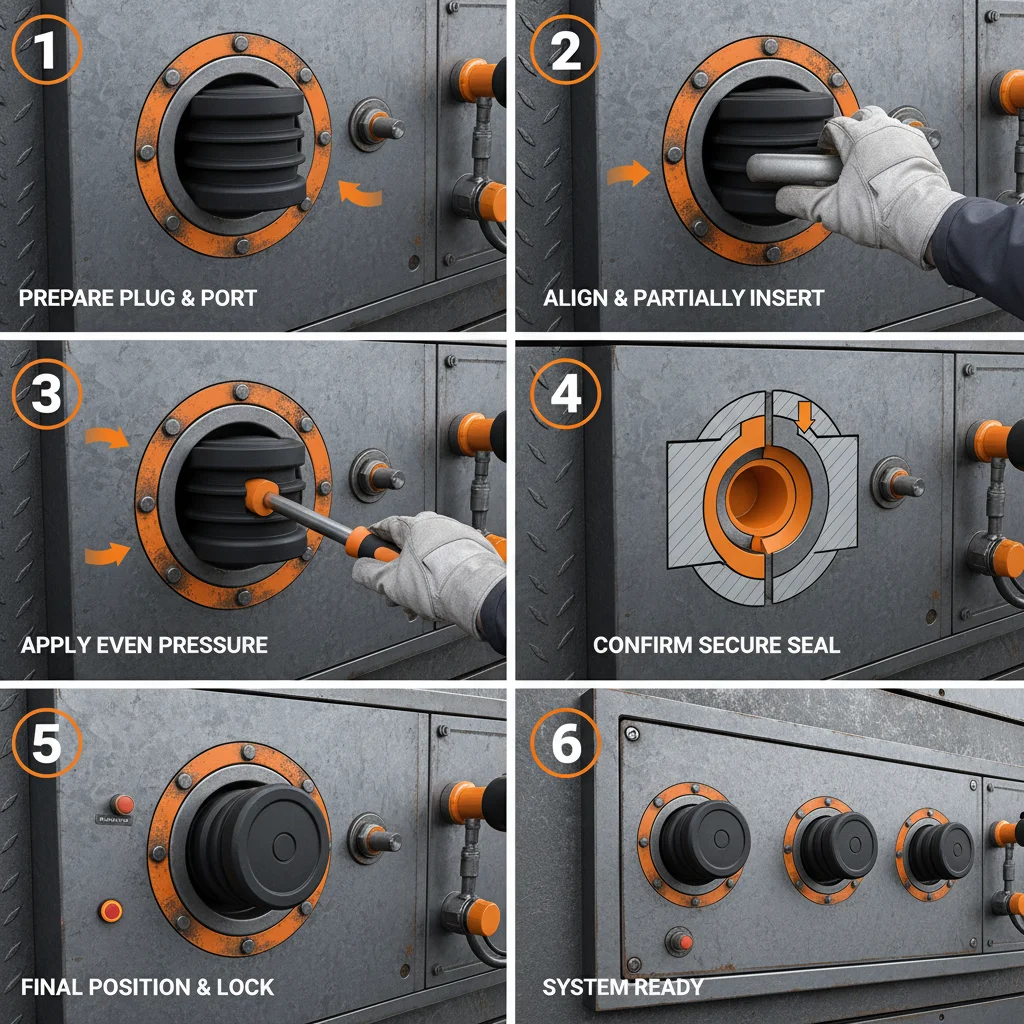
Finally, the installation method determines the longevity of the seal. Whether it is a press-fit or a seated arrangement, the seal must be installed without twisting or tearing. Proper integration into the mechanical equipment ensures that the specified temperature and pressure limits are respected, preventing premature wear and tear.
Performance Metrics and Material Efficiency
Evaluating the performance of sealing solutions requires a quantitative approach. Key metrics include the compression set, which measures the rubber's ability to return to its original thickness after prolonged stress, and the leak rate under varying pressures. By analyzing these data points, engineers can predict the lifespan of the seal and schedule preventative maintenance.
Efficiency is not only about the seal's performance but also about the manufacturing process. The use of precision molds allows for rapid production with minimal material waste, ensuring that each unit meets the tight tolerances required for industrial applications. This balance of high-performance output and cost-effective production is what makes these components viable for mass-market mechanical equipment.
Comparative Performance of Various Sealing Methods
Global Applications and Sector Use Cases
The application of Mechanical Rubber Seals spans almost every modern industry. In the food and beverage sector, silicone-based seals ensure that production lines remain hygienic and compliant with health codes, preventing the growth of bacteria in seal gaps. Meanwhile, in the automotive industry, these seals are critical for maintaining engine oil levels and preventing transmission fluid leaks.
Beyond commercial use, these seals are vital in extreme environments. In remote mining operations or offshore oil rigs, the seals must withstand saltwater corrosion and extreme temperature swings. In these contexts, the reliability of a simple rubber ring can be the difference between a successful operation and a catastrophic environmental spill.
Long-Term Value and Sustainability
Investing in high-quality rubber seals provides tangible long-term value by reducing the frequency of replacement and the risk of unplanned outages. While lower-grade seals may seem cost-effective initially, their shorter lifespan leads to higher cumulative costs and more frequent labor expenses for installation. A premium seal, engineered for the specific fluid and temperature of the system, offers a far superior return on investment.
From a sustainability perspective, the move toward more durable materials reduces the amount of rubber waste entering landfills. Furthermore, by preventing oil and gas leaks, these seals play a direct role in protecting the environment. The precision of a well-designed labyrinth gap reduces the loss of expensive lubricants, contributing to a more resource-efficient industrial process.
Ultimately, the value of a seal is measured by trust. When a technician installs a component, they trust that the seal will hold under pressure. This trust is built on rigorous testing—such as 100% pre-delivery testing—ensuring that every part leaving the factory is capable of performing its duty without failure.
Future Trends in Sealing Technology
The future of Mechanical Rubber Seals is being shaped by the digital transformation of manufacturing. "Smart seals" are being explored, incorporating sensors that can alert operators when a seal is nearing the end of its life or when a leak is detected in real-time. This shift from preventative to predictive maintenance will revolutionize how factories manage their assets.
Material science is also evolving with the introduction of nano-composites. These new materials offer unprecedented resistance to heat and chemicals, allowing rubber seals to be used in applications previously reserved for expensive metal-to-metal seals. The integration of bio-based rubbers is also gaining traction, reducing the reliance on petroleum-based polymers and aligning with global green energy goals.
Automation in the production process, including 3D printing of custom seal prototypes, is significantly shortening the lead time for custom rubber parts. This allows for rapid iteration and optimization of seal geometry, ensuring that the labyrinth gap is perfectly tuned for the specific mechanical equipment it serves.
Comparison of Rubber Seal Material Properties for Industrial Use
| Material Type |
Temp Resistance |
Chemical Stability |
Typical Application |
| Food Grade Silicone |
High |
Excellent |
Food/Medical |
| Nitrile (NBR) |
Medium |
Good (Oil) |
Automotive Oil |
| Viton (FKM) |
Very High |
Superior |
Chemical Plants |
| EPDM |
High |
Good (Water) |
Outdoor Piping |
| Neoprene |
Medium |
Moderate |
General Industrial |
| Custom Composite |
Variable |
Tailored |
Specialized Machinery |
FAQS
Delivery times vary based on stock availability. Products in stock can be delivered within 1 workday. If the product is out of stock but the mold is available, it typically takes 5-7 workdays. If both the product and mold are out of stock, delivery generally takes 10-15 workdays, depending on the total order quantity.
Yes, these seals are specifically engineered to function under both static and moving conditions. They maintain a secure seal under specified temperature and pressure ranges, making them suitable for a wide variety of mechanical equipment, whether the part is stationary or rotating.
Absolutely. Our metric colored silicone rubber o-rings are food-grade, meaning they are produced using materials that meet the strict safety and non-toxicity standards required for food and beverage applications, preventing any harmful contamination of the product.
We offer flexible shipping via Express, Air, or Sea to accommodate different urgency and budget needs. For payments, we welcome a wide range of options including Cash, Credit Card, T/T, Paypal, and Western Union to ensure a smooth transaction process for our global clients.
Quality assurance is a core part of our process. We perform a 100% test on all products before delivery to ensure they meet all specified parameters and dimensions. Additionally, our packaging (PE bag inside, Carton outside, Pallet) is designed to protect the seals during transit.
Yes, we can supply samples for parts we have ready in stock. While the sample itself may be free in some cases, customers are generally responsible for the sample cost and the courier shipping fees to verify the fit and quality before committing to a large order.
Conclusion
Mechanical Rubber Seals are far more than simple rubber rings; they are precision-engineered components that safeguard the efficiency and safety of global industrial infrastructure. By integrating advanced materials like food-grade silicone and utilizing a labyrinth design to prevent leaks, these seals resolve the critical challenge of maintaining fluid integrity in the most demanding environments. From the initial material selection to the final 100% quality test, every step in their production is geared toward reliability and long-term durability.
As we look toward the future, the integration of smart sensing and sustainable polymers will further enhance the role of sealing technology in the digital factory. For businesses seeking to minimize downtime and maximize the lifespan of their mechanical equipment, investing in high-specification, custom-tailored seals is the most effective strategy. We invite you to explore our comprehensive range of sealing solutions to find the perfect fit for your technical requirements. Visit our website: www.beikesealing.com