In the demanding world of industrial sealing, the integrity of a system often depends on the smallest components. High-performance sealing solutions are essential for preventing leaks and ensuring the operational safety of machinery exposed to harsh chemical environments. Among these, the role of specialized elastomers is critical in maintaining vacuum and pressure stability across various sectors.
The global demand for precision-engineered seals has grown as industries push the boundaries of temperature and pressure. Whether in petroleum extraction or pharmaceutical manufacturing, the ability of a seal to resist degradation when in contact with hydrocarbons is a non-negotiable requirement. Without the correct material selection, equipment failure can lead to costly downtime and significant safety hazards.
To address these challenges, engineers rely on Oil Resistant O-Rings to provide a reliable barrier against fluid migration. These components are engineered from advanced materials like NBR, FKM, and HNBR to ensure that seals remain flexible and intact even under continuous exposure to oils and fuels.

Material Composition of Oil Resistant O-Rings
The effectiveness of these seals begins with the selection of the base polymer. For standard oil resistance, Nitrile Butadiene Rubber (NBR) is the industry benchmark due to its excellent balance of cost and performance. However, for more aggressive chemical environments or higher temperatures, materials like Fluorocarbon (FKM/VITON) and Hydrogenated Nitrile (HNBR) are employed to prevent the elastomer from swelling or hardening.
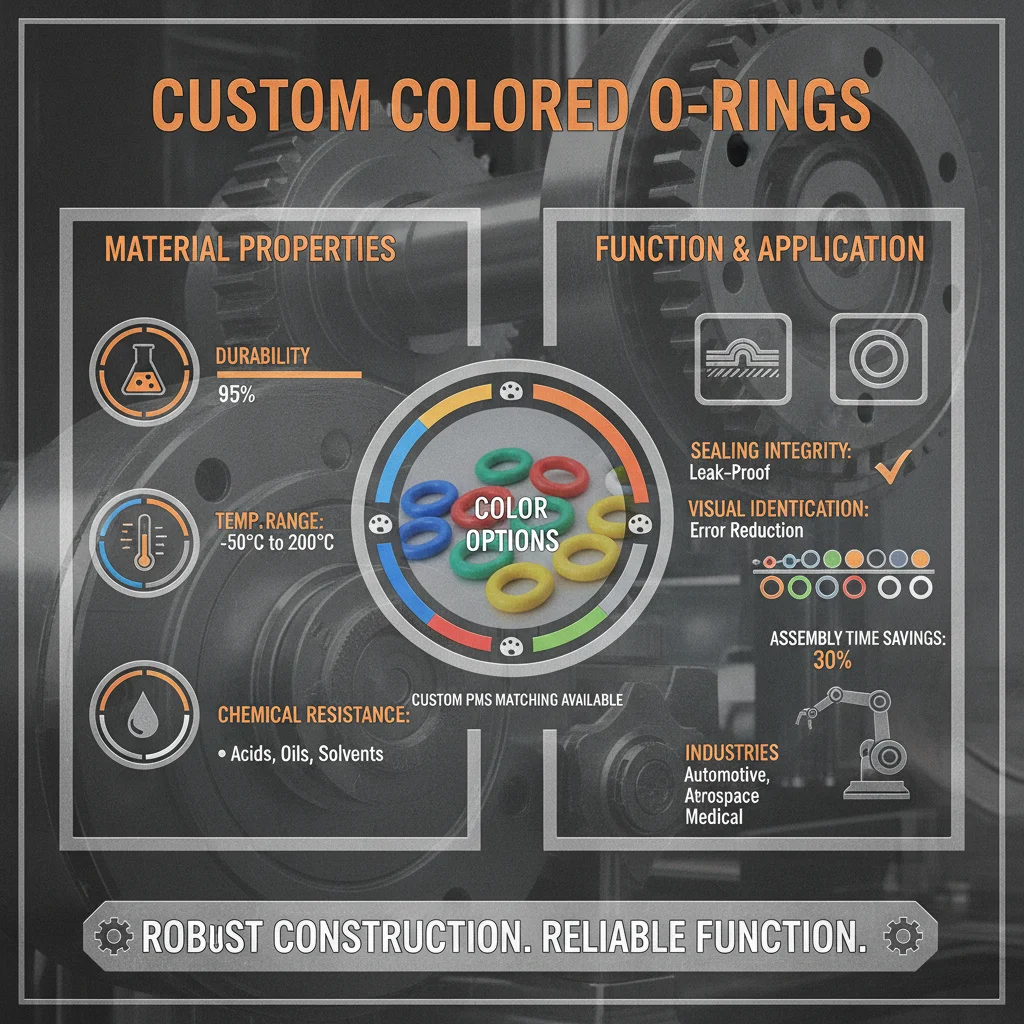
Beyond the base polymer, the addition of specific curing agents and fillers ensures that the final product maintains its structural integrity. These additives optimize the elasticity and hardness—typically around 70 Shore A—allowing the seal to conform perfectly to the groove and maintain a tight seal under varying pressures.
Core Technical Performance Factors
One of the primary factors in evaluating sealing performance is thermal stability. Different materials offer varying working temperature ranges; for instance, NBR typically handles -40°C to 120°C, while FKM can withstand temperatures up to 200°C. This range is critical because excessive heat can lead to thermal degradation, while extreme cold can cause the seal to lose its elasticity and leak.
Chemical and ozone resistance are equally vital. In environments where seals are exposed to atmospheric ozone or corrosive chemicals, the elastomer must resist "cracking" or surface degradation. The use of high-quality raw materials ensures that the seal provides an effective barrier against acids and alkaline substances, extending the service life of the equipment.
Mechanical durability, including wear resistance and compression set, determines how long a seal will function before requiring replacement. A low compression set means the material returns to its original shape after being compressed, which is essential for maintaining a constant sealing force over years of operation in hydraulic and pneumatic systems.
Global Industrial Applications
The versatility of Oil Resistant O-Rings makes them indispensable across a multitude of global industries. In the petroleum and chemical sectors, these seals are used in reaction vessels, heat exchangers, and boilers where they must withstand a constant barrage of hydrocarbons and corrosive agents.
In the automotive and heavy machinery industries, these components are integrated into excavators and engine systems to prevent lubricant leaks. The ability to maintain a seal under high-pressure dynamic conditions ensures that machinery operates efficiently even in remote industrial zones or harsh outdoor environments.
Beyond heavy industry, the medical and food sectors utilize specialized grades of these seals. While oil resistance is a primary focus, these applications often require food-grade silicone or encapsulated materials to ensure that the sealing process does not contaminate the product, maintaining strict hygiene standards.
Comparative Analysis of Sealing Efficiency
When selecting a sealing solution, engineers must weigh the trade-offs between cost, temperature limits, and chemical compatibility. While a basic NBR seal is cost-effective for low-temperature oil applications, it fails in high-heat scenarios where FKM is required. Understanding this hierarchy is key to avoiding premature seal failure and reducing maintenance overhead.
By analyzing the performance ratings of different elastomer types, companies can optimize their procurement process. The goal is to find the "sweet spot" where the material exceeds the environmental requirements without unnecessary over-specification, thereby balancing budget with operational reliability.
Performance Rating of Various Oil Resistant O-Rings Materials
Long-Term Value and Reliability
Investing in high-quality Oil Resistant O-Rings provides tangible long-term value by drastically reducing the frequency of unscheduled maintenance. When a seal is correctly matched to its medium, the risk of leaks is minimized, which in turn prevents environmental contamination and ensures the safety of the workforce.
From a logical perspective, the cost of a premium seal is negligible compared to the cost of a system-wide shutdown. Reliability builds trust in the equipment's performance, allowing operators to push machines to their full capacity without the constant fear of seal rupture or fluid loss.
Future Innovations in Elastomer Technology
The future of sealing technology is moving toward "smart materials" and sustainable polymers. Research is focusing on developing elastomers that can signal their own wear and tear or that possess self-healing properties when subjected to minor abrasions. This shift will move the industry from reactive maintenance to a truly predictive model.
Sustainability is also playing a larger role. The development of bio-based elastomers that maintain the same oil resistance as synthetic rubbers is a priority for companies aiming to reduce their carbon footprint. These green alternatives aim to provide the same durability while being more environmentally friendly during the production phase.
Additionally, the integration of additive manufacturing (3D printing) for custom rubber parts allows for the creation of complex geometries that were previously impossible. This enables the design of seals that can adapt to irregular surfaces, further improving the efficiency of leakage prevention in specialized machinery.
Material Selection Guide for Harsh Environments
Choosing the right material is a scientific process that requires understanding the specific chemical interaction between the fluid and the polymer. For most standard oil applications, NBR provides a reliable and cost-effective solution. However, if the system involves high-temperature steam or aggressive fuel additives, moving toward FKM or FFKM is the only way to ensure longevity.
Environmental factors such as UV exposure and ozone levels also dictate the choice. EPDM is excellent for weather resistance but fails in oil contact, whereas NBR is excellent for oil but weaker against ozone. This is why a detailed analysis of the working environment is the first step in any successful sealing project.
By utilizing a standardized selection matrix, procurement managers can ensure consistency in quality across different product lines. This systematic approach eliminates guesswork and ensures that every seal installed meets the rigorous standards of ISO9001 and TS16949.
Material Compatibility and Performance Matrix for Oil Resistant Sealing
| Material Type |
Oil Resistance Level |
Max Temp (°C) |
Typical Application |
| NBR (Nitrile) |
High |
120 |
General Hydraulics |
| FKM (Viton) |
Extreme |
200 |
Chemical Plants |
| HNBR |
Very High |
150 |
Auto Engine Seals |
| Silicone |
Low |
230 |
Medical/Food Grade |
| EPDM |
Very Low |
150 |
Water/Steam Systems |
| FFKM |
Absolute |
320 |
Semiconductor Fab |
FAQS
For high-heat environments, FKM (Viton) or FFKM are the best choices. FKM can typically handle temperatures up to 200°C while maintaining excellent resistance to hydrocarbons. FFKM is used for the most extreme cases, reaching up to 320°C and providing near-universal chemical resistance.
NBR is excellent for most petroleum-based oils and fuels. However, it may not be suitable for applications involving polar solvents, ketones, or extremely high temperatures. For these specific cases, switching to FKM or HNBR is recommended to prevent seal swelling.
Common signs of failure include visible swelling (the seal becomes larger and softer), hardening (the seal becomes brittle and cracks), or a loss of elasticity. If the seal no longer "springs back" after compression, it has likely degraded and needs replacement.
Yes, specialized food-grade silicone or encapsulated rubber seals are used in the food and medical industries. These are designed to be oil-resistant while complying with safety certifications to ensure no toxic substances leach into the product.
Shore A is a measure of the hardness of the rubber. 70 Shore A is the industry standard for most O-rings, providing a balance between being soft enough to create a seal and hard enough to resist extrusion under pressure.
The best way to extend seal life is to ensure the material is correctly matched to the operating temperature and chemical medium. Additionally, proper installation (avoiding twisting or cutting the seal) and maintaining the correct lubrication levels can significantly prevent premature wear.
Conclusion
Maintaining the integrity of industrial systems requires a meticulous approach to sealing. From the selection of NBR for standard use to the deployment of FFKM for extreme conditions, Oil Resistant O-Rings serve as the first line of defense against leakage and equipment failure. By understanding the relationship between polymer composition, thermal limits, and chemical compatibility, companies can ensure operational safety and efficiency.
As we move toward a future of smarter, more sustainable materials, the importance of precision sealing will only grow. We encourage engineers and procurement specialists to prioritize material certification and technical compatibility over short-term cost savings to achieve long-term reliability. For high-quality, custom sealing solutions, visit our website: www.beikesealing.com