In the complex world of industrial sealing, the demand for reliable, oil-resistant components is paramount to maintaining operational efficiency. NBR O-Rings serve as a cornerstone in this domain, providing a critical barrier that prevents the leakage of essential lubricants and protects internal machinery from harmful contaminants. By utilizing Nitrile Butadiene Rubber, these seals ensure that mechanical systems can operate under demanding pressures without failure.
Globally, the manufacturing and automotive sectors rely heavily on high-performance elastomers to reduce downtime and maintenance costs. The ability of a seal to withstand harsh chemical environments while maintaining its structural integrity is what separates a standard component from an industrial-grade solution. As industries push toward higher efficiency and tighter tolerances, the precision engineering behind these sealing rings becomes increasingly vital.
Selecting the appropriate material is not merely a technical choice but a strategic decision that impacts the lifespan of the entire equipment. For those seeking durable, oil-resistant solutions, NBR O-Rings offer the perfect balance of elasticity and chemical strength, making them indispensable for both static and dynamic sealing applications across various mechanical environments.

The Fundamental Composition of NBR O-Rings
NBR O-Rings are annular covers consisting of one or more parts, specifically engineered to form a narrow labyrinth gap. This design allows the seal to be fixed on a ring or washer of a bearing, effectively contacting another ring to create a leak-proof barrier. The primary goal is to prevent the leakage of oil while simultaneously blocking foreign objects from entering the sensitive internal components of the machinery.
The material used—Nitrile Butadiene Rubber—is chosen specifically for its exceptional resistance to oil and fuel. This chemical composition ensures that the seal does not swell or degrade when exposed to petroleum-based products, which is a common failure point for other rubber materials. Consequently, these rings are the preferred choice for industrial areas where oil contact is constant.
Industrial Significance and Global Demand
The global industrial landscape relies heavily on the precision of rubber seals to maintain the integrity of hydraulic and pneumatic systems. In an era where ISO standards dictate the quality of mechanical output, the role of NBR O-Rings has shifted from being a simple consumable to a critical component of system reliability. Without these seals, the risk of environmental contamination and mechanical failure would increase exponentially.
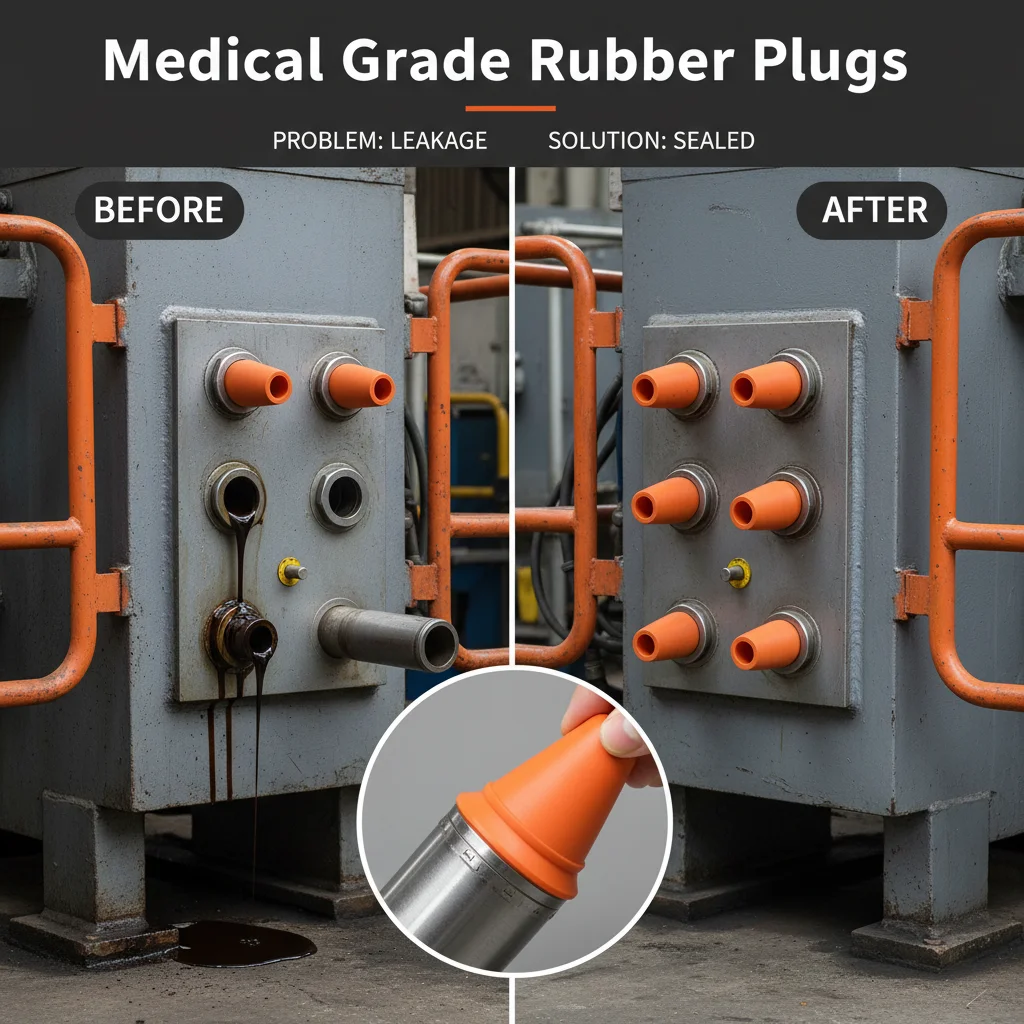
Many industries face the challenge of "leakage-induced downtime," where a single failed seal can stop an entire production line. This is particularly evident in heavy manufacturing and automotive assembly, where high-pressure oil systems are ubiquitous. The demand for high-quality NBR seals is driven by the need to minimize these costly interruptions through the use of materials that offer predictable wear patterns and high durability.
Furthermore, the versatility of these rings allows them to be utilized in both static and moving conditions. Whether they are sealing a stationary joint or a rotating shaft, their ability to adapt to the specified temperature and pressure makes them a universal solution. This adaptability is why they are found in everything from simple household appliances to complex aerospace equipment.
Key Material Properties and Selection Criteria
When evaluating the effectiveness of NBR O-Rings, the primary focus is usually on their chemical compatibility. Nitrile rubber is renowned for its excellent resistance to oils, which makes it superior to general-purpose rubbers like NR (Natural Rubber) in industrial settings. However, the selection process must be rigorous to ensure the material matches the environmental stressors.
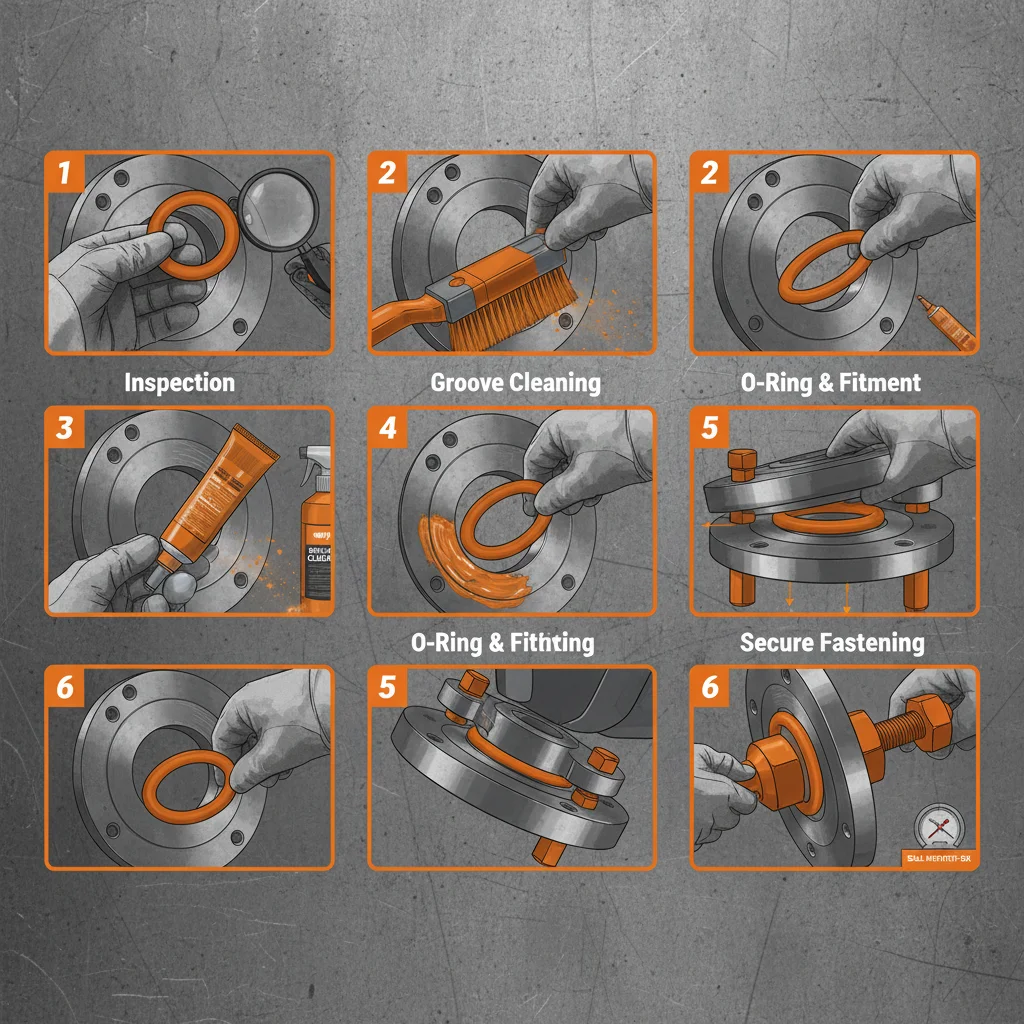
To select the right NBR O-Rings, engineers must ask critical questions: What medium will the seal contact (oil, chemicals, or water)? What is the maximum and minimum application temperature? Is the seal intended for a dynamic or static application, and will it be a surface seal or a shaft seal? These factors determine whether NBR is the optimal choice or if a material like FKM or Silicone is required.
Beyond chemical resistance, physical properties such as compression set and elasticity play a vital role. A high-quality seal must be able to return to its original shape after being compressed, ensuring a tight seal over thousands of cycles. This mechanical resilience is what allows NBR to perform reliably under varying pressures and temperatures.
Performance Metrics in Diverse Environments
Evaluating the performance of sealing materials requires a look at how they react to different catalysts and stressors. NBR is specifically optimized for oil-rich environments, but its performance can vary depending on the specific grade of the rubber and the temperature of the medium it is sealing. Understanding these metrics helps in predicting the maintenance lifecycle of the equipment.
For instance, while NBR excels in oil resistance, it may not be the best choice for extreme weather or ozone exposure compared to EPDM. By analyzing the trade-offs between elasticity, heat resistance, and chemical strength, operators can maximize the uptime of their machinery and avoid premature seal failure.
Performance Rating of NBR O-Rings vs Other Materials
Global Applications and Use Cases
In real-world industrial contexts, these seals are deployed across a vast array of sectors. From the hydraulic systems of construction machinery in remote mining zones to the precision valves of pharmaceutical factories, the application of these seals is universal. Their ability to work under both static and moving conditions makes them ideal for fuel pumps, engine gaskets, and hydraulic cylinders.
Beyond heavy industry, they are also critical in specialized environments. For example, in oil and gas extraction, where equipment is exposed to aggressive hydrocarbons, the chemical stability of the Nitrile material prevents catastrophic leaks that could lead to environmental disasters or workplace accidents. This makes the reliable sourcing of these components a matter of safety and environmental responsibility.
Long-Term Value and Operational Reliability
The long-term value of investing in high-quality rubber seals lies in the reduction of Total Cost of Ownership (TCO). While lower-grade seals might be cheaper upfront, their propensity for premature failure leads to increased labor costs and lost production revenue. High-standard NBR seals provide a logical and emotional peace of mind, knowing that the system is secure.
Reliability also manifests as safety. In high-pressure pneumatic systems, a seal failure is not just a leak; it can be a safety hazard for operators. By ensuring that seals are manufactured to strict tolerances and tested 100% before delivery, manufacturers provide a level of trust that is essential for critical infrastructure.
Sustainability is another key angle. Seals that last longer mean fewer replacements and less rubber waste ending up in landfills. By optimizing the material for the specific working condition—such as the exact temperature and medium—industries can move toward a more sustainable, "fit-for-purpose" maintenance model.
Future Trends in Elastomeric Sealing
The future of the sealing industry is moving toward "Smart Sealing" and advanced material hybridization. We are seeing a trend where standard rubber is combined with nano-materials to enhance thermal conductivity or increase wear resistance. This evolution will allow seals to operate in even more extreme environments without sacrificing the flexibility that Nitrile provides.
Automation and digital transformation are also playing a role. With the advent of predictive maintenance, seals may eventually be integrated with sensors that alert operators before a failure occurs. This shift from reactive to proactive replacement will revolutionize how industrial plants manage their spare parts inventory and scheduling.
Green energy transitions are also prompting the development of new elastomers that can handle bio-fuels and synthetic lubricants. As the world moves away from traditional petroleum, the chemistry of rubber seals must evolve to remain compatible with these new, often more corrosive, green alternatives.
Comparative Analysis of Rubber Materials for Sealing Applications
| Material Type |
Primary Strength |
Ideal Medium |
Reliability Score |
| NBR |
Oil Resistance |
Industrial Oils/Fuel |
9/10 |
| EPDM |
Weather/Ozone Resistance |
Outdoor/Heat |
8/10 |
| FKM (Viton) |
High Temp/Chemicals |
Aggressive Acids |
10/10 |
| Silicone |
Temp Range |
Food/Medical |
7/10 |
| CR (Neoprene) |
Mechanical Properties |
General Purpose |
7/10 |
| HNBR |
Thermal Stability |
High-Heat Oil |
9/10 |
FAQS
The primary advantage is their superior oil and fuel resistance. While natural rubber (NR) may degrade or swell when exposed to petroleum products, Nitrile rubber is specifically engineered to maintain its shape and sealing integrity in oil-rich environments, making it the industry standard for mechanical equipment.
You should analyze the working conditions: the contact medium (oil, seawater, or solvents), the application temperature, and whether the seal is static or dynamic. We recommend consulting with a material expert to identify the most cost-effective material that meets your specific pressure and temperature requirements.
NBR is excellent for moderate temperatures, but for extreme heat, materials like FKM (Viton) or Silicone are better. If you need oil resistance combined with higher thermal stability, HNBR (Hydrogenated Nitrile) is often the suggested alternative to standard NBR.
Delivery depends on stock and molds. In-stock products ship in 1 workday. If the mold is in stock but the product isn't, it takes 5-7 workdays. For entirely new molds and products, delivery typically ranges from 10-15 workdays, depending on the order quantity.
We implement a rigorous quality control process where 100% of the seals undergo testing before delivery. This ensures that every ring meets the specified dimensions and material hardness, preventing failures upon installation in your equipment.
We offer flexible shipping via Express, Air, or Sea to accommodate various urgency levels. Payment is highly accessible, accepting Cash, Credit Cards, T/T, Paypal, and Western Union to facilitate smooth global transactions.
Conclusion
In summary, NBR O-Rings represent a critical intersection of material science and mechanical engineering. By providing unmatched oil resistance and structural durability, they protect the heartbeat of industrial machinery, ensuring that leaks are prevented and operational efficiency is maximized. From the selection of the correct elastomer to the precision of the final mold, every detail contributes to the reliability of the system.
Looking forward, the continued evolution of rubber compounds and the integration of smart monitoring will further enhance the lifespan of these components. For businesses aiming to reduce downtime and increase safety, investing in high-grade, tested sealing solutions is not just a maintenance necessity—it is a strategic advantage. Visit our website for more professional sealing solutions: www.beikesealing.com