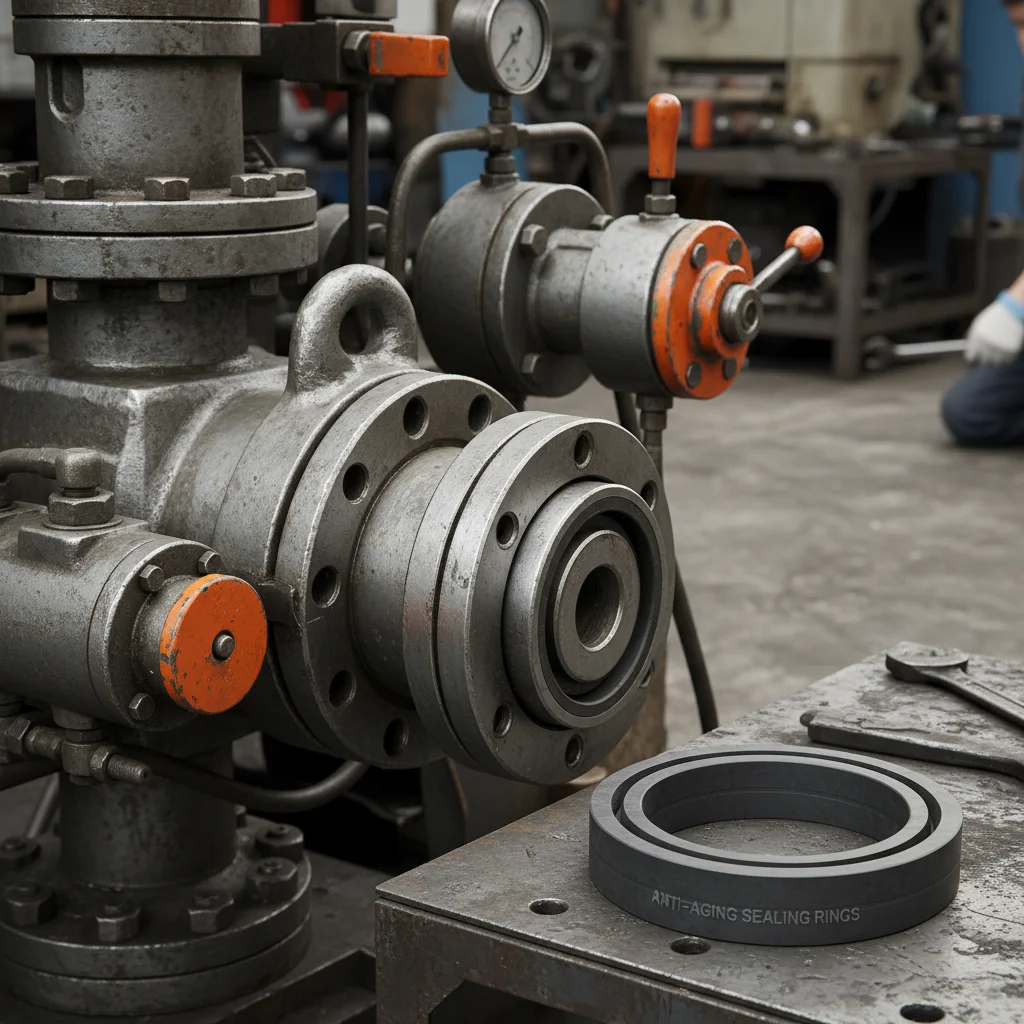
Electrical equipment seals serve as the critical first line of defense for sensitive electronic components, preventing the ingress of moisture, dust, and corrosive contaminants. In an era where automation and high-voltage systems are ubiquitous, the reliability of these sealing solutions determines the operational lifespan and safety of the entire electrical infrastructure. By creating an airtight and watertight barrier, these components ensure that internal circuitry remains isolated from harsh environmental stressors.
The global demand for high-performance sealing materials has surged as industries transition toward greener energy and more complex semiconductor manufacturing. Whether it is protecting a transformer in a coastal region or ensuring the integrity of a medical device, the material science behind these seals is evolving to meet extreme temperature and chemical requirements. Failure to implement the correct sealing strategy often leads to catastrophic short circuits or premature equipment degradation, highlighting the necessity of precision engineering.
Understanding the nuances of material selection, from NBR to FFKM, is essential for engineers seeking to optimize their systems. By integrating high-quality Electrical Equipment Seals, companies can significantly reduce maintenance downtime and enhance the overall safety of their electrical installations across various industrial sectors.

The Critical Role of Material Selection in Electrical Sealing
Choosing the right elastomer is the most pivotal decision when designing seals for electrical components. For instance, Nitrile (NBR) is often selected for its excellent resistance to petroleum-based oils and fuels, making it ideal for equipment used in automotive or industrial machinery. However, when the environment involves extreme heat or aggressive chemicals, Flouroelastomers (FKM) or Perflouroelastomers (FFKM) are required due to their superior thermal stability and chemical inertness.
Moreover, the hardness of the material, typically ranging from 5 to 90 Shore A, must be balanced against the compression set requirements of the application. A seal that is too hard may not create a sufficient leak-proof interface, while one that is too soft may deform under pressure, leading to failure. This delicate balance ensures that the seal maintains its integrity over thousands of thermal cycles.
Defining Electrical Equipment Seals in Modern Industry
In technical terms, electrical equipment seals are specialized elastomeric components designed to isolate electrical conductors, insulators, and circuitry from the external environment. These can range from simple O-rings and gaskets to complex custom-molded rubber parts. Their primary function is to prevent the entry of water, dust, and hazardous gases, which could otherwise cause dielectric breakdown or oxidation of critical contacts.
Beyond simple protection, these seals often play a role in vibration dampening and mechanical stabilization. In high-voltage environments, the ability of a seal to maintain its physical properties without becoming conductive or brittle is paramount. This makes the use of certified materials, such as those adhering to ISO9001 and IATF16949 standards, a non-negotiable requirement for industrial safety.
In the context of the global supply chain, these components are the "silent guardians" of infrastructure. From the semiconductor cleanrooms to aerospace control panels, the precision of the seal's dimensions—often dictated by strict customer drawings—ensures that the equipment can operate in conditions that would otherwise be uninhabitable for electronic components.
Core Components of High-Performance Sealing Systems
The effectiveness of Electrical Equipment Seals depends on several core factors, primarily durability and chemical compatibility. Durability refers to the material's ability to withstand environmental degradation, such as UV exposure or ozone attack, which is why EPDM is frequently utilized for outdoor electrical enclosures due to its excellent weather resistance.
Another critical aspect is thermal range. Silicone (VMQ) is highly prized in the electrical industry because it can operate in temperatures as low as -90ºF and as high as 430ºF. This wide operating window allows Electrical Equipment Seals to be used in everything from cryogenic sensors to high-heat industrial furnaces without losing their elasticity.
Finally, the precision of the molding process ensures that the seal fits perfectly within its groove. Whether utilizing standard sizes or custom designs, the tolerance of the part prevents "blow-by" or leak paths. This engineering precision is what allows semiconductor equipment to maintain the ultra-pure environments required for wafer fabrication.
Evaluating Performance Metrics for Industrial Seals
To determine the efficacy of a sealing solution, engineers use a variety of metrics including compression set, tensile strength, and permeability. A low compression set is particularly important for electrical enclosures, as it indicates that the rubber will return to its original shape after being compressed, ensuring a long-term seal against moisture ingress.
Comparing different materials allows for a cost-benefit analysis. While FFKM offers the highest level of chemical resistance and thermal stability, its cost is significantly higher than NBR or EPDM. The goal is to match the material properties exactly to the environment's demands to avoid over-engineering while ensuring total reliability.
Performance Comparison of Sealing Materials
Global Applications Across High-Tech Sectors
The application of these sealing solutions is diverse, spanning from the aerospace industry to household appliances. In the aerospace sector, seals must withstand rapid pressure changes and extreme temperature fluctuations, requiring high-grade FKM or specialized HNBR. These materials ensure that avionics and electrical control systems remain functional during ascent and descent through various atmospheric layers.
In the semiconductor and photovoltaic industries, the requirements are even more stringent. For example, the high-temperature diffusion furnaces used in solar cell production require seals capable of withstanding 300-400℃. This necessitates the use of FFKM or advanced silicone blends to prevent contamination of the silicon wafers, which would otherwise result in massive production losses.
Long-Term Value and Reliability Advantages
The primary long-term value of investing in premium sealing solutions is the drastic reduction in Total Cost of Ownership (TCO). While a cheap NBR seal might be sufficient for a short period, its failure in a corrosive environment leads to expensive equipment replacement and unplanned downtime. High-quality seals extend the mean time between failures (MTBF), providing peace of mind for facility managers.
From a safety perspective, the reliability of electrical seals is directly linked to the prevention of fires and electrical shocks. By maintaining a strict barrier against moisture, these components prevent the formation of conductive paths (tracking) across insulators. This trust in the material's integrity allows for the deployment of electrical equipment in more challenging environments, such as offshore wind farms or deep-sea mining operations.
Furthermore, the use of RoHS and LFGB certified materials ensures that the seals are environmentally sustainable and safe for use in food-grade electrical equipment. This adherence to international standards not only ensures compliance but also enhances the brand reputation of the equipment manufacturer by demonstrating a commitment to quality and safety.
Future Trends in Smart Sealing Technologies
As we move toward Industry 4.0, the integration of "smart" materials into sealing technology is becoming a reality. Future iterations of seals may incorporate conductive fillers or embedded sensors that can signal when a seal is beginning to degrade or leak. This shift from reactive to predictive maintenance will revolutionize how electrical grids and industrial plants are managed.
Sustainability is also driving innovation. The development of bio-based elastomers that offer the same performance as petroleum-derived NBR or FKM is a key area of research. Reducing the carbon footprint of the manufacturing process, while maintaining the strict tolerances required for electrical applications, is the next great challenge for the rubber industry.
Additionally, the rise of electric vehicles (EVs) is creating a surge in demand for seals that can handle the unique thermal and chemical environment of battery packs and high-voltage charging stations. This requires a hybrid approach, combining the chemical resistance of fluorinated rubbers with the lightness and flexibility of advanced silicones.
Comparative Analysis of Material Suitability for Electrical Environments
| Material Type |
Temp Range |
Key Electrical Use Case |
Durability Score (1-10) |
| NBR (Nitrile) |
-40ºF to 250ºF |
Standard Control Boxes |
6 |
| EPDM |
-60ºF to 300ºF |
Outdoor Power Distribution |
8 |
| FKM (Viton) |
0ºF to 390ºF |
High-Temp Avionics |
9 |
| Silicone (VMQ) |
-90ºF to 430ºF |
Medical Device Electronics |
8 |
| HNBR |
-40ºF to 300ºF |
EV Battery Cooling Seals |
9 |
| FFKM |
0ºF to 600ºF |
PV Diffusion Furnaces |
10 |
FAQS
The choice depends on your primary environmental stressor. If your equipment is exposed to petroleum oils, fuels, or aggressive solvents, FKM is the superior choice due to its chemical inertness. However, if your primary concern is an extreme temperature range (particularly very low temperatures) or food-grade compliance, Silicone is the better option. Always review the specific chemical compatibility chart for your operating environment.
Lifespan varies wildly based on material and environment. An NBR seal in a mild indoor environment may last 5-10 years, while an EPDM seal outdoors may last 7-12 years. In extreme high-heat scenarios, even FKM may need replacement every 2-3 years. To maximize lifespan, ensure the seal is not over-compressed and that the mating surfaces are clean and free of burrs.
Yes, significantly. Standard O-rings may not provide a perfect fit for complex geometries, leading to "leak paths." Custom-molded seals are designed based on your exact CAD drawings to ensure optimal compression and a complete seal. This can improve the IP (Ingress Protection) rating of your enclosure, reducing the need for expensive internal heating or dehumidifying elements.
Professional manufacturers like Shijiazhuang Beike Sealing Technology provide seals that are fully compliant with ISO9001, IATF16949, and ROHS. This ensures that the materials are free from hazardous substances and that the production process is consistent. Compliance is critical for companies exporting electrical equipment to European or North American markets.
A seal with a hardness that is too high may fail to "conform" to the irregularities of the mating surface. This creates microscopic gaps that allow moisture or dust to enter. Additionally, an overly hard seal requires significantly more clamping force to achieve a seal, which can lead to the warping of the electrical enclosure or the stripping of fasteners.
Most professional suppliers offer free samples for the first order of new customers. This allows engineers to perform "fit-and-function" tests and verify material compatibility in a real-world setting before committing to a large production run of 10,000+ pieces. Testing samples is highly recommended to avoid costly errors in mass production.
Conclusion
In summary, the integrity of electrical systems is fundamentally dependent on the quality and precision of their sealing components. From the initial selection of materials like FKM, Silicone, or FFKM to the rigorous adherence to ISO and IATF standards, every detail contributes to the safety and longevity of the equipment. By focusing on the synergy between material science and precise engineering, industries can prevent costly failures and ensure seamless operation in the most demanding environments.
Looking ahead, the shift toward sustainable materials and smart, sensor-integrated seals will further enhance the reliability of our global electrical infrastructure. For engineers and procurement specialists, the key to success lies in partnering with a manufacturer that offers both technical design support and a diverse material laboratory. To ensure your equipment is protected by the best in the industry, visit our website: www.beikesealing.com.