In the demanding world of industrial sealing, selecting the right elastomer is critical to preventing leaks and ensuring operational safety. EPDM O-Rings have emerged as a cornerstone solution for environments where traditional rubber fails, offering a unique balance of resilience and chemical stability. By providing a reliable seal against fluids and gases, these components protect expensive machinery and prevent hazardous environmental contamination.
The global demand for high-performance seals is driven by the expansion of the automotive, aerospace, and food processing sectors. As industries shift toward more sustainable and durable materials, the role of ethylene propylene diene monomer (EPDM) has expanded due to its exceptional ability to withstand extreme weather and oxidative stress. Understanding the technical nuances of these seals is essential for engineers aiming to reduce maintenance costs and extend the lifecycle of their equipment.
Whether you are dealing with high-temperature steam or outdoor exposure to UV radiation, choosing high-quality EPDM O-Rings ensures that your systems remain airtight and efficient. By leveraging advanced molding techniques and certified materials, manufacturers can provide customized sealing solutions that meet rigorous international standards like ISO9001 and IATF16949.

Material Composition and Properties of EPDM O-Rings
Ethylene Propylene Diene Monomer (EPDM) is a synthetic rubber known for its exceptional versatility. The material composition of EPDM O-Rings allows them to maintain a flexible structure while resisting the degrading effects of ozone and sunlight. This makes them far superior to natural rubber in outdoor settings where atmospheric oxidation typically causes cracking and premature failure.
Beyond weather resistance, the mechanical properties of these rings are highly customizable. Depending on the application, hardness can be adjusted from 5 to 90 Shore A, ensuring that the seal provides enough compression to prevent leaks while remaining elastic enough to recover its shape after the load is removed.
Temperature Resistance and Thermal Stability
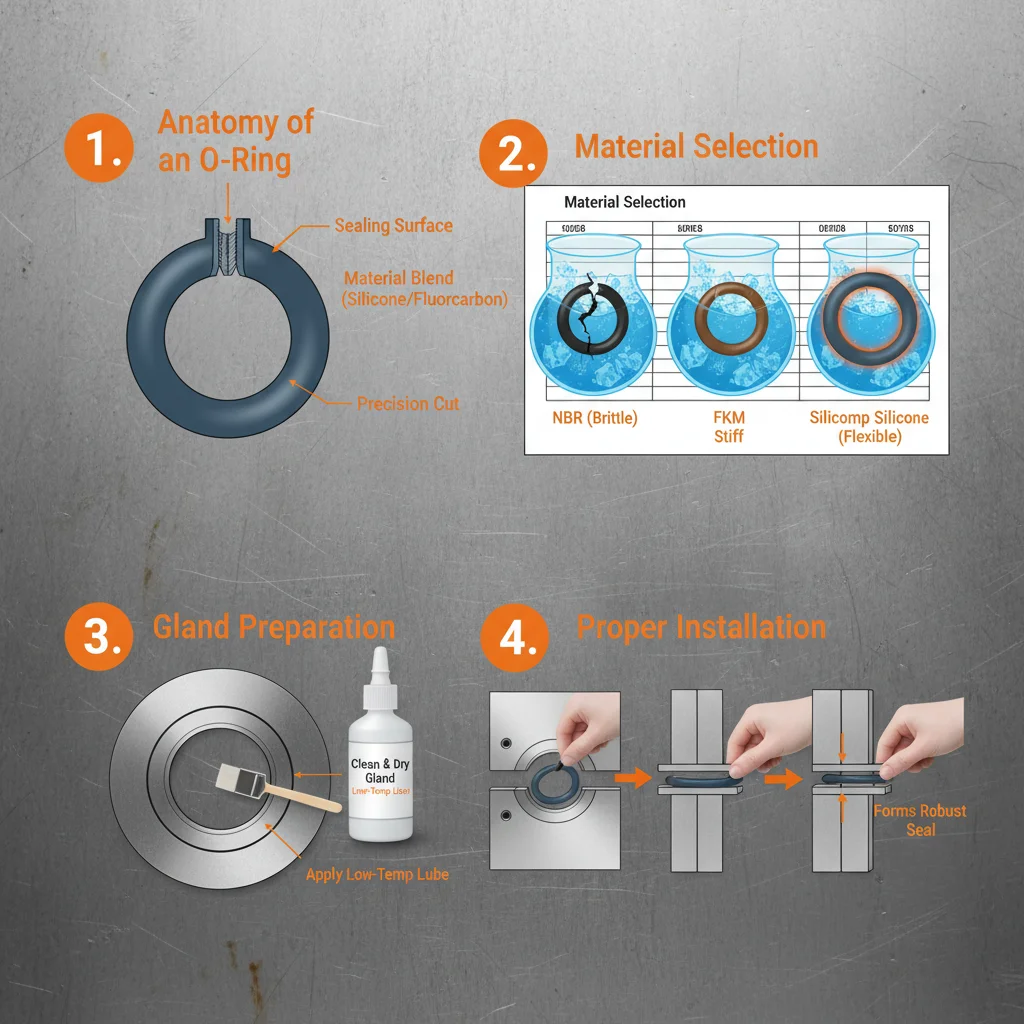
One of the most significant advantages of EPDM is its wide operational temperature range. These seals are designed to function effectively from as low as -60ºF up to 300ºF. This thermal stability ensures that the seal does not become brittle in freezing conditions or soften excessively under high heat, maintaining a consistent seal integrity.
In industrial steam applications, the ability to resist thermal degradation is paramount. Unlike Nitrile (NBR), which may harden and crack when exposed to high-temperature steam, EPDM maintains its molecular stability. This makes it the primary choice for boiler systems, autoclaves, and other heat-exchange equipment.
The ability to withstand extreme temperature fluctuations without losing elasticity prevents "compression set," a common failure mode where a seal permanently flattens. By resisting this deformation, EPDM ensures a long-term leak-proof barrier in fluctuating thermal environments.
Chemical Compatibility and Environmental Resistance
Understanding the chemical compatibility of EPDM O-Rings is essential for preventing material swelling or degradation. These seals are exceptionally resistant to polar substances, including ketones, dilute acids, and alkalis. This makes them ideal for use in pharmaceutical and food-grade environments where cleaning agents are frequently used.
However, it is critical to note that EPDM O-Rings are not compatible with petroleum-based oils, gasoline, or diesel fuels. Exposure to hydrocarbons causes the rubber to swell and lose its physical strength, leading to total seal failure. For oil-rich environments, materials like FKM or NBR should be considered instead.
In addition to chemical resistance, the ozone resistance of EPDM O-Rings is world-class. Because the polymer chain lacks the unstable double bonds found in natural rubber, it does not react with atmospheric ozone, ensuring that seals installed in outdoor infrastructure remain intact for years without cracking.
Performance Metrics in Industrial Applications
Evaluating the performance of sealing solutions requires a look at several key metrics, including compression set, tensile strength, and elongation. EPDM excels in applications where high recovery is needed. When compressed in a groove, the material's "push-back" force ensures that the seal remains tight even if there is slight vibration or mechanical shifting.
From a cost-efficiency perspective, EPDM provides a middle-ground solution. While it is more expensive than basic natural rubber, it is significantly more affordable than high-end fluoroelastomers like FFKM, offering a high ROI for applications that require weather and steam resistance but not extreme chemical inertness.
Performance Comparison of EPDM Sealing Solutions
Global Application Standards and Use Cases
EPDM seals are utilized globally across a diverse array of sectors. In the automotive industry, they are indispensable for window seals, door weatherstripping, and brake fluid systems, where their resistance to brake fluids and outdoor elements is critical for passenger safety and comfort.
In the food and beverage industry, food-grade EPDM is used in piping and valves to ensure that no contaminants enter the production line. Because they can withstand the aggressive steam cleaning (SIP - Sterilization In Place) processes common in pharmaceutical plants, they are the gold standard for maintaining hygienic environments.
Manufacturing Process and Quality Control
The production of high-quality seals begins with precise compounding. In our raw material laboratory, polymers are mixed with curing agents and fillers to achieve specific hardness and elasticity levels. This ensures that every batch of seals maintains consistency in its physical properties.
Moulding is the core process, where the rubber is heated and pressed into high-precision molds. Whether producing standard sizes or custom drawings, the use of IATF16949 and ISO9001 certified processes ensures that tolerances are kept within microns, preventing leaks that could result from improper fitment.
Final quality control involves rigorous inspection, including hardness testing and dimensional verification. By adhering to ROHS and LFGB standards, we ensure that the materials are safe for their intended use, particularly in medical and food-contact applications.
Comparative Analysis of Elastomer Selection
Choosing the right material requires a trade-off analysis. For instance, while Silicone offers higher temperature resistance, it lacks the mechanical tear strength and abrasion resistance of EPDM. Therefore, for dynamic seals exposed to the elements, EPDM is the superior choice.
Compared to Nitrile (NBR), EPDM is the clear winner for outdoor and steam use, whereas NBR is necessary for oil-based hydraulic systems. Understanding these differences prevents costly downtime and equipment failure caused by using the wrong elastomer for the environment.
For extreme high-temperature or aggressive chemical environments, FFKM (Perfluoroelastomer) is the ultimate solution, though it comes at a significantly higher cost. For most general-purpose weather and steam applications, EPDM remains the most cost-effective and reliable option available.
Comparative Material Analysis for Sealing Applications
| Material Type |
Temp Range |
Oil Resistance |
Weather/Steam |
| EPDM |
-60ºF to 300ºF |
Poor |
Excellent |
| NBR (Nitrile) |
-40ºF to 250ºF |
Excellent |
Fair |
| FKM (Viton) |
-22ºF to 428ºF |
Excellent |
Good |
| VMQ (Silicone) |
-90ºF to 430ºF |
Fair |
Excellent |
| HNBR |
-40ºF to 300ºF |
Excellent |
Good |
| FFKM |
0ºF to 600ºF |
Universal |
Universal |
FAQS
No, EPDM is not suitable for petroleum-based hydraulic oils. Exposure to hydrocarbons causes the rubber to swell and lose its structural integrity, which will lead to seal failure. For hydraulic applications, we recommend NBR (Nitrile) or FKM (Fluoroelastomer) depending on the temperature and pressure requirements.
EPDM is widely regarded as the best general-purpose rubber for steam. It can typically handle temperatures up to 300ºF. Its ability to resist thermal degradation in moist, high-heat environments makes it ideal for autoclaves and industrial boilers where other elastomers would harden and leak.
If the seal is in direct contact with food, beverages, or pharmaceuticals, you must use a food-grade version of EPDM. These are manufactured without harmful plasticizers and comply with standards such as LFGB or FDA. Using non-food-grade rubber in these applications can lead to chemical leaching and regulatory non-compliance.
EPDM has a saturated polymer backbone, which means it is naturally resistant to ozone and UV radiation. NBR contains unsaturated bonds that react with ozone in the air, leading to "ozone cracking." This is why EPDM is preferred for window seals, automotive weatherstripping, and outdoor infrastructure.
Yes, we specialize in both standard sizes and custom designs. Our engineering team can help you optimize the cross-section and diameter of your seals based on your specific application drawings. We provide OEM and ODM services to ensure the seal fits perfectly within your hardware.
We offer a wide range of hardness levels, typically from 5 to 90 Shore A. Soft seals (lower Shore A) are ideal for low-pressure applications or fragile mating surfaces, while harder seals (higher Shore A) are used for high-pressure environments to prevent the seal from extruding into the gap.
Conclusion
In summary, EPDM O-Rings represent an essential component in modern industrial sealing, offering unparalleled resistance to weather, ozone, and high-temperature steam. By balancing mechanical durability with chemical stability in polar environments, they provide a reliable and cost-effective solution for the automotive, pharmaceutical, and aerospace industries. Choosing the correct hardness and grade—whether standard or food-grade—is the key to ensuring system longevity and operational safety.
As industry demands move toward higher efficiency and sustainability, the importance of precision-engineered elastomers will only grow. We encourage engineers and procurement managers to prioritize certified materials and rigorous quality control to avoid the high costs of seal failure. For professional consultation or custom sealing solutions, visit our website: www.beikesealing.com.